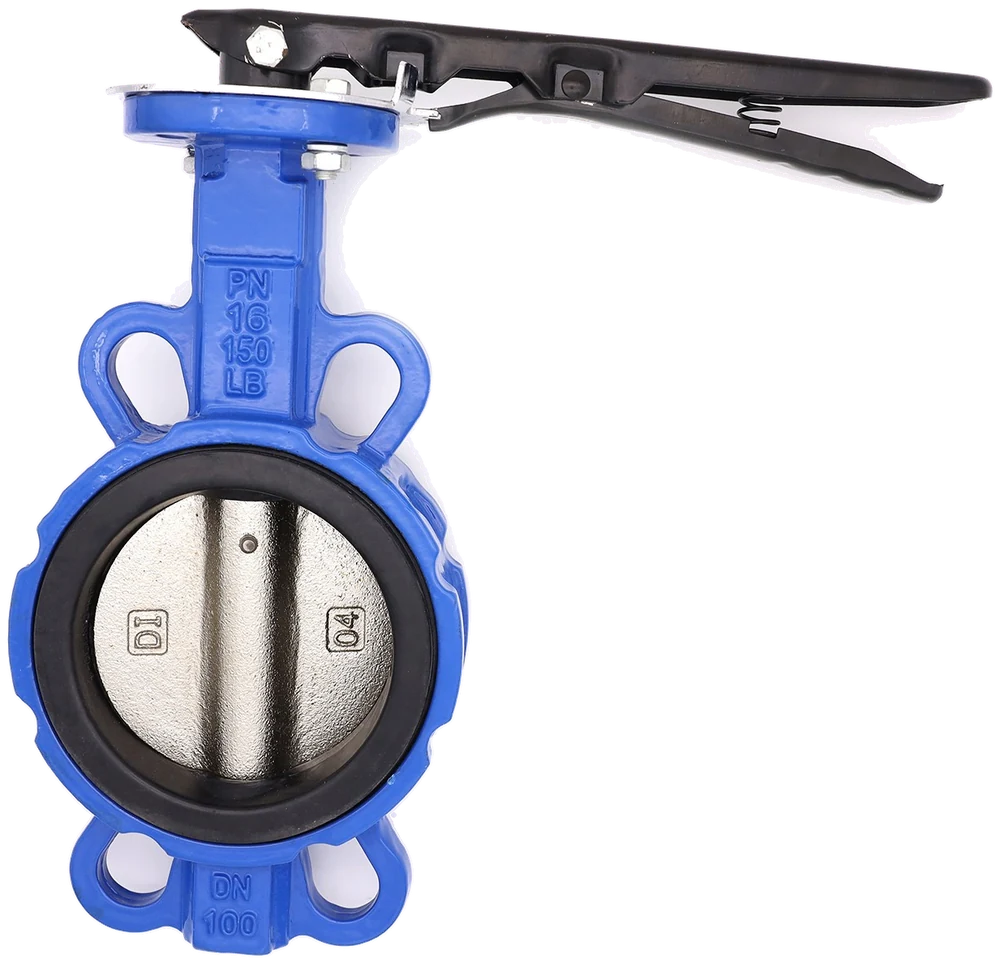
 72
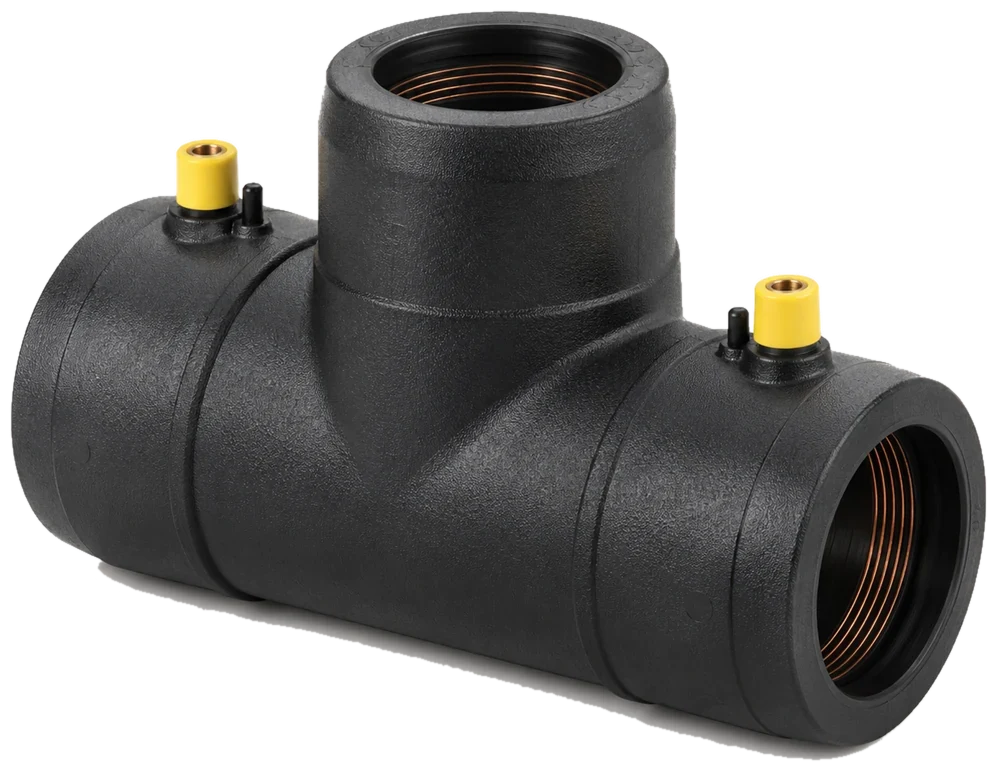 38
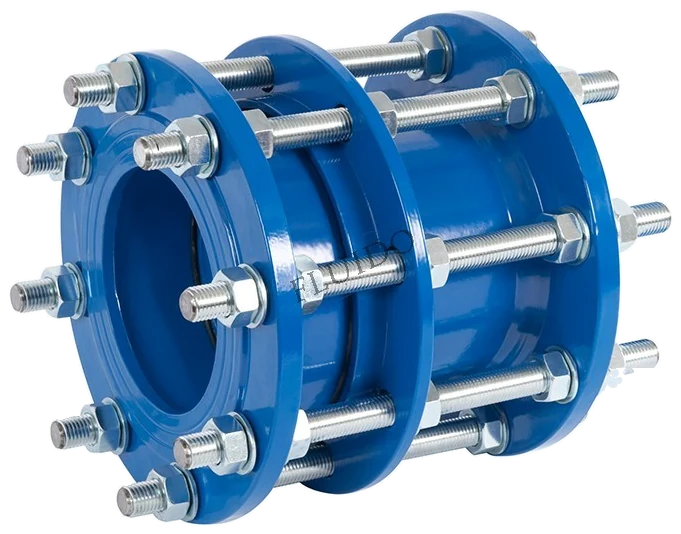 32
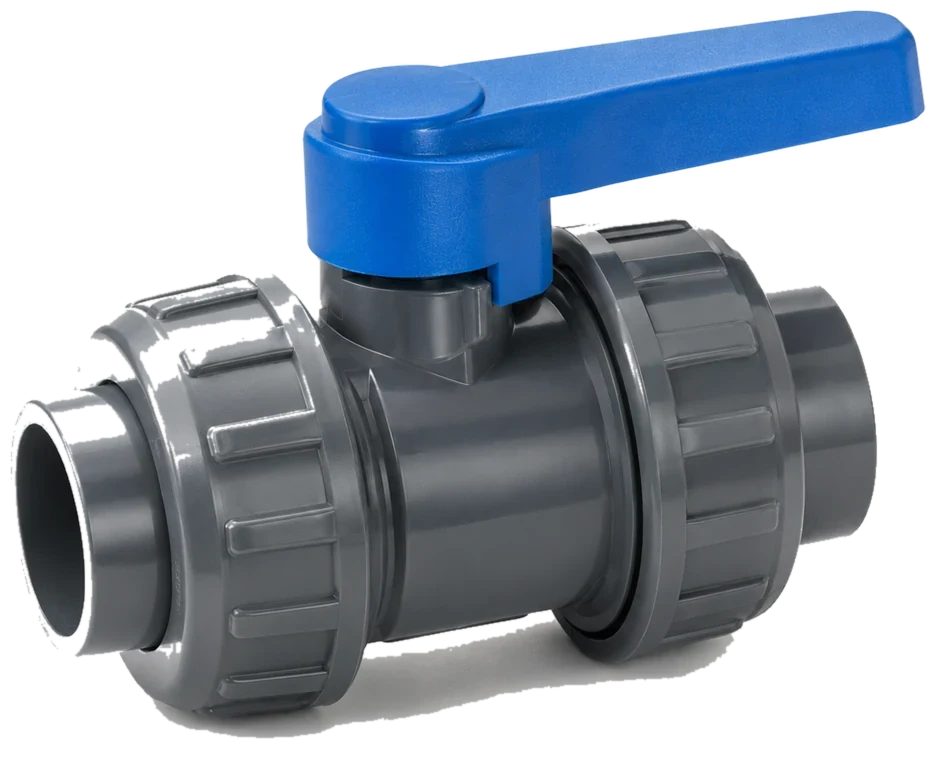 21
 15
 9
Quality starts before production.
Agree material, dimensions, rating and documents in the order. Inspection scope is defined for each product and factory.
- Specification
- Drawing and applicable standard
- Verification
- Agreed acceptance criteria
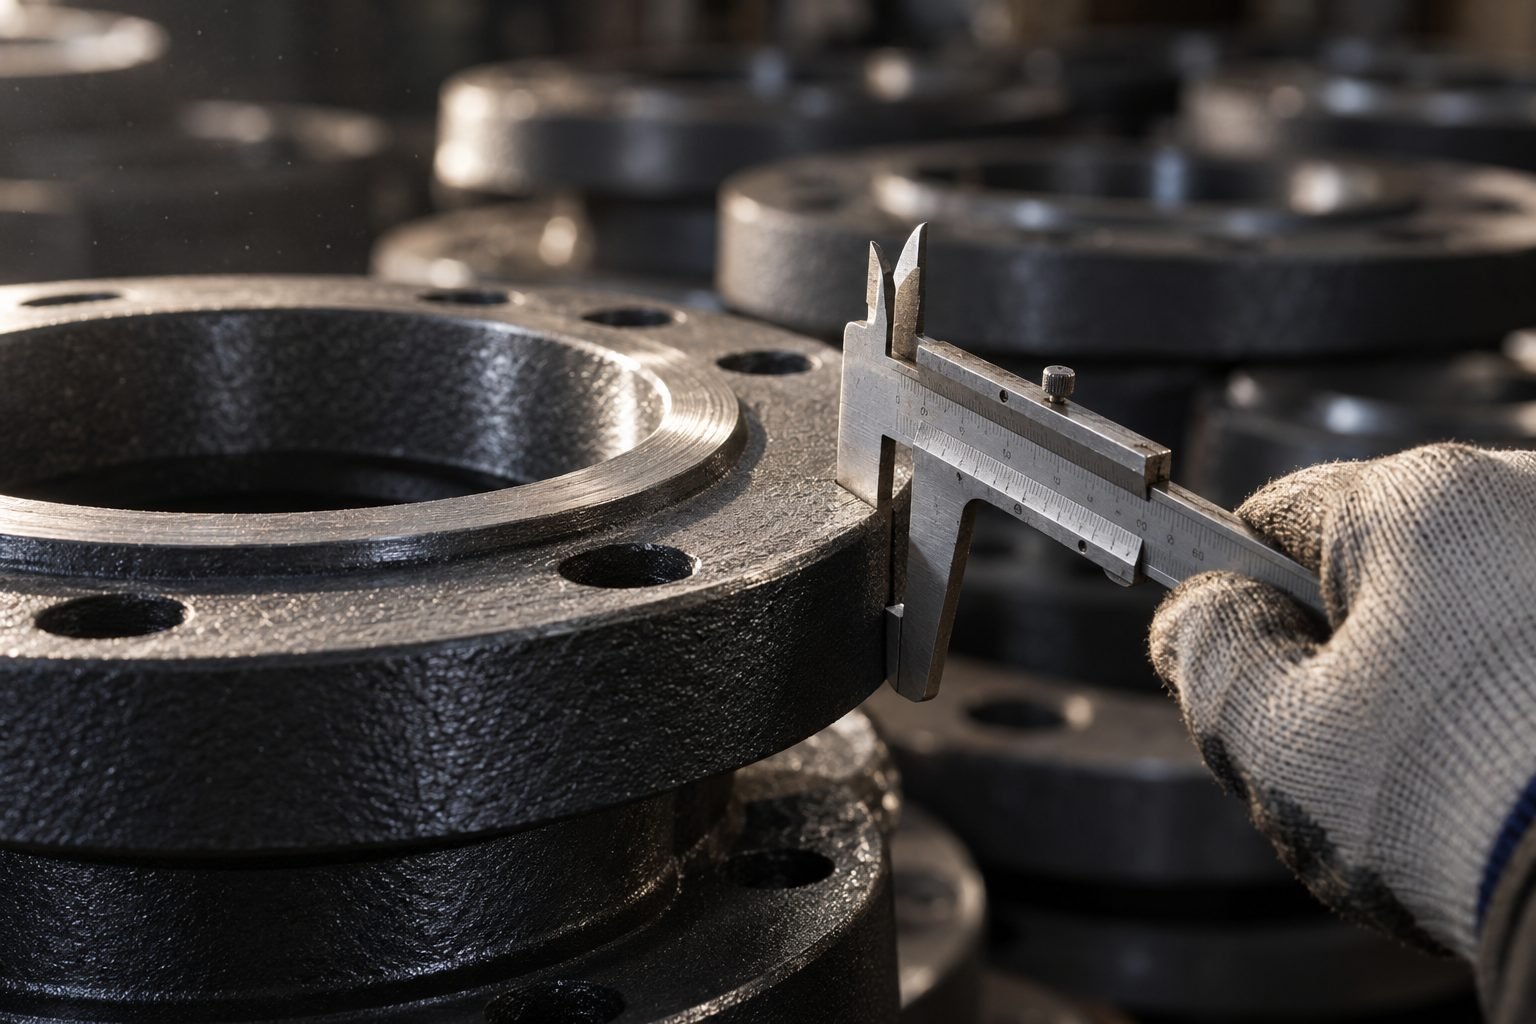
Match each part to its factory.
Selection starts with the process: casting, machining, moulding or fusion. Before confirmation, we review the available technical information against the material list.
- Before ordering
- Model, material and standard
- If certification is required
- Request the document and its current scope
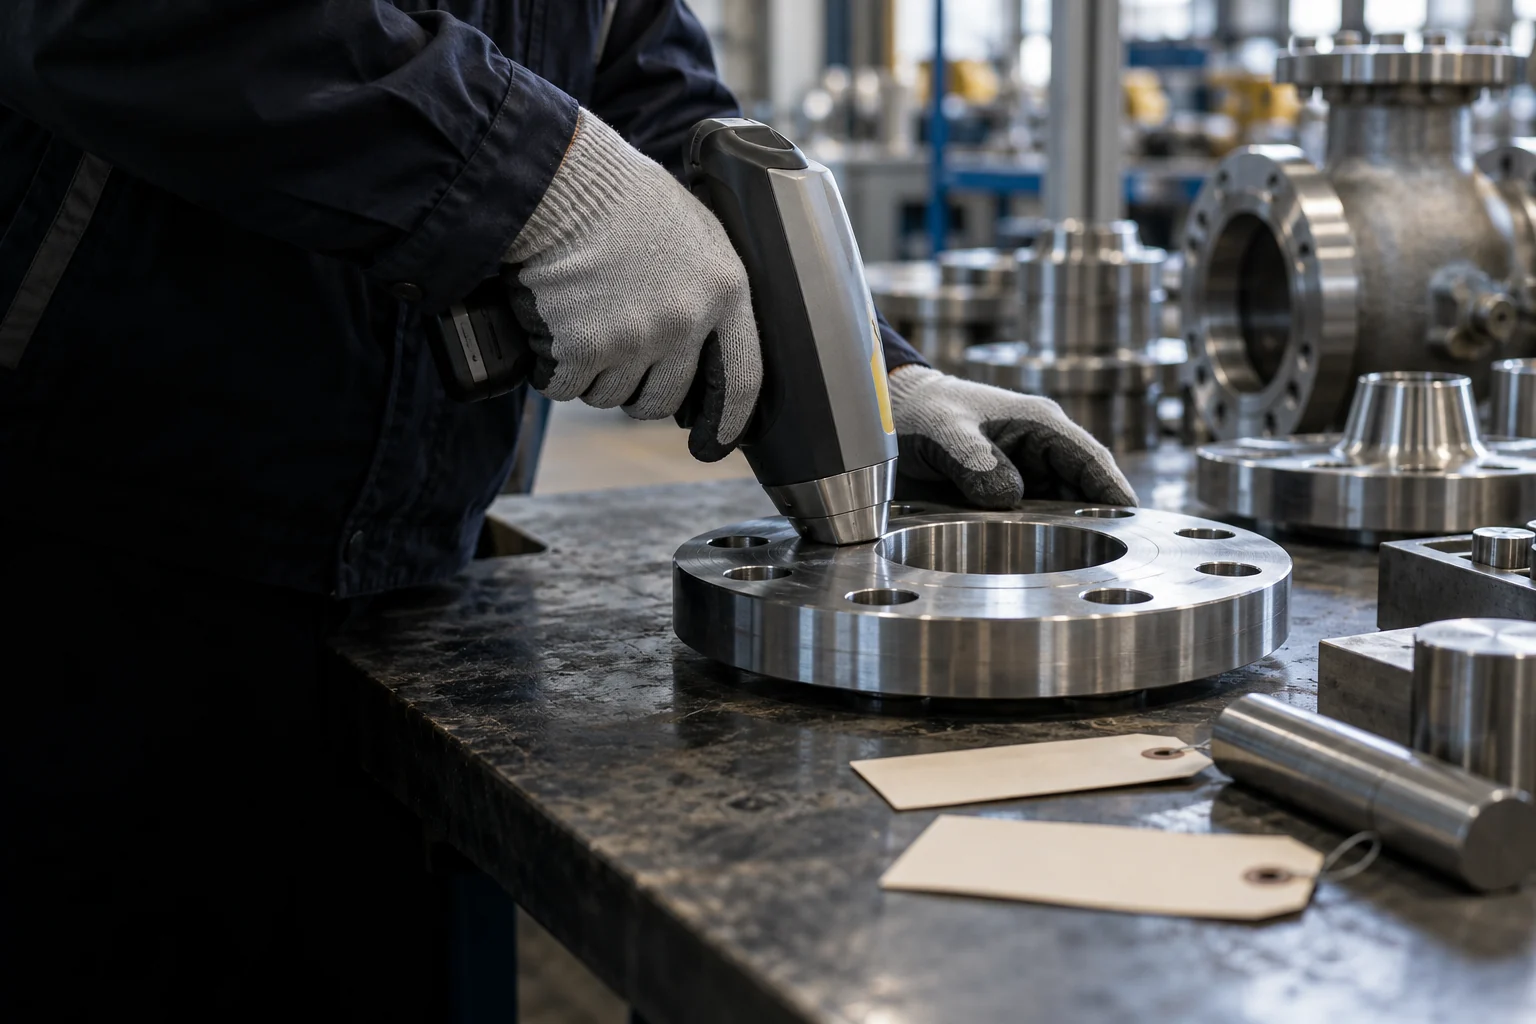
Material needs identity and traceability.
Ductile iron, stainless and carbon steel need different checks. Specify any material analysis or certificate required by the project in the quotation request.
- Body and internals
- Specify each material separately
- Batch
- Agree identification and documents
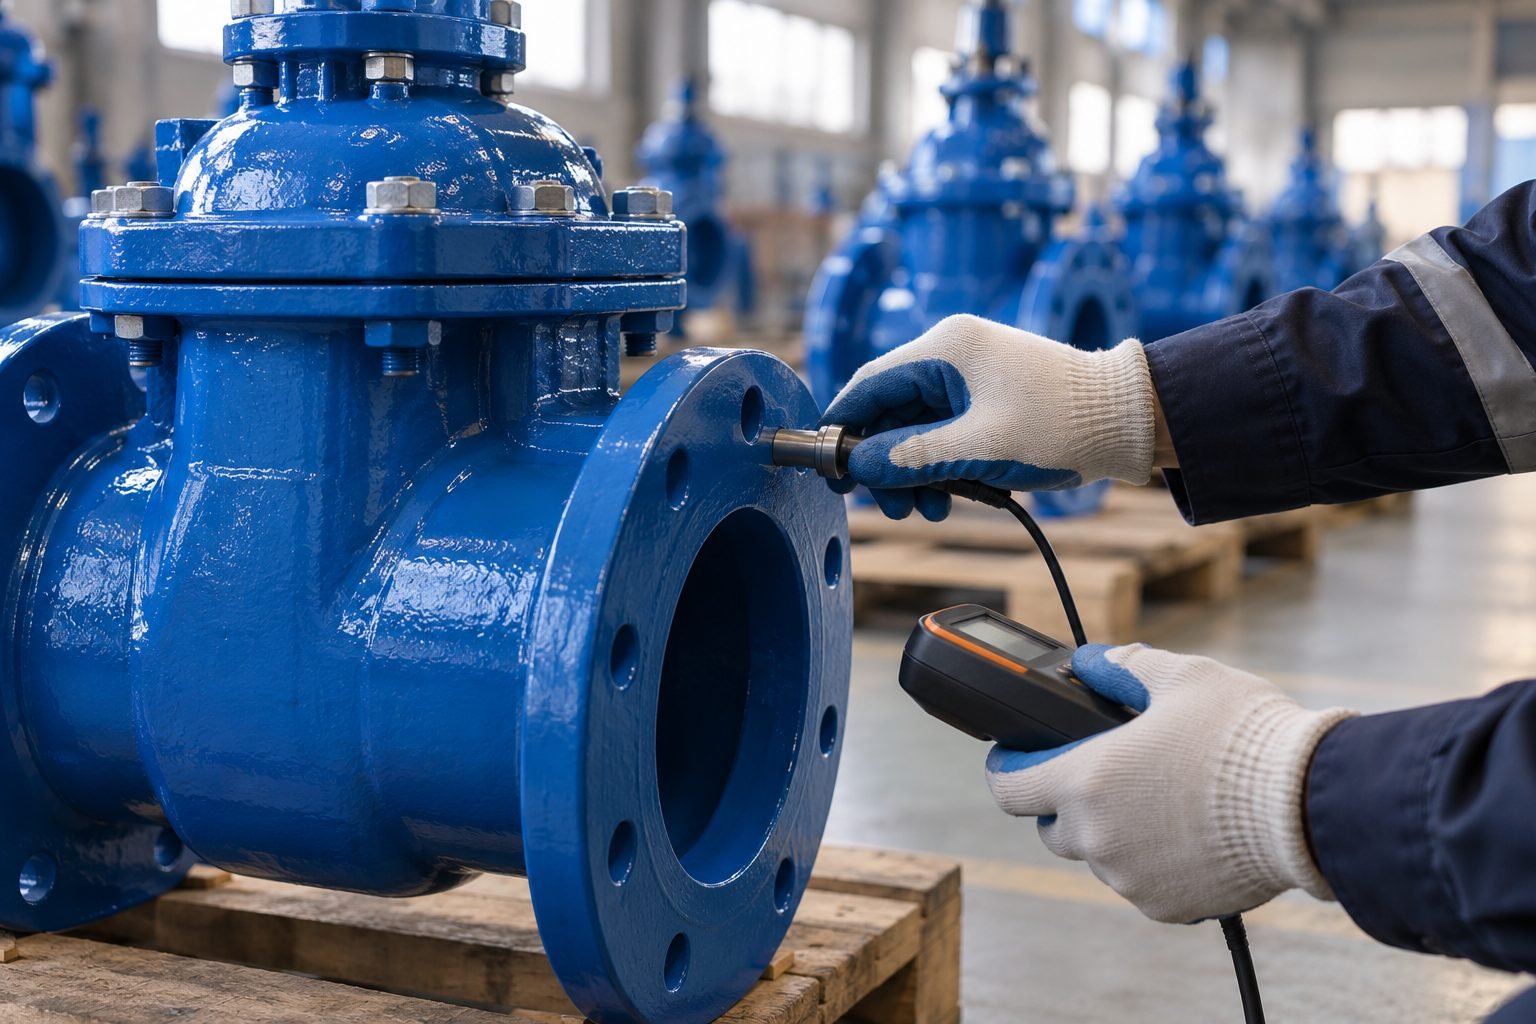
The connection must fit the installation.
Check size, face-to-face length, drilling and flange facing against the specification. Agree coating and acceptance criteria for the service.
- Flanges
- Standard, DN/NPS and PN/Class
- Coating
- Type, thickness and surfaces to inspect
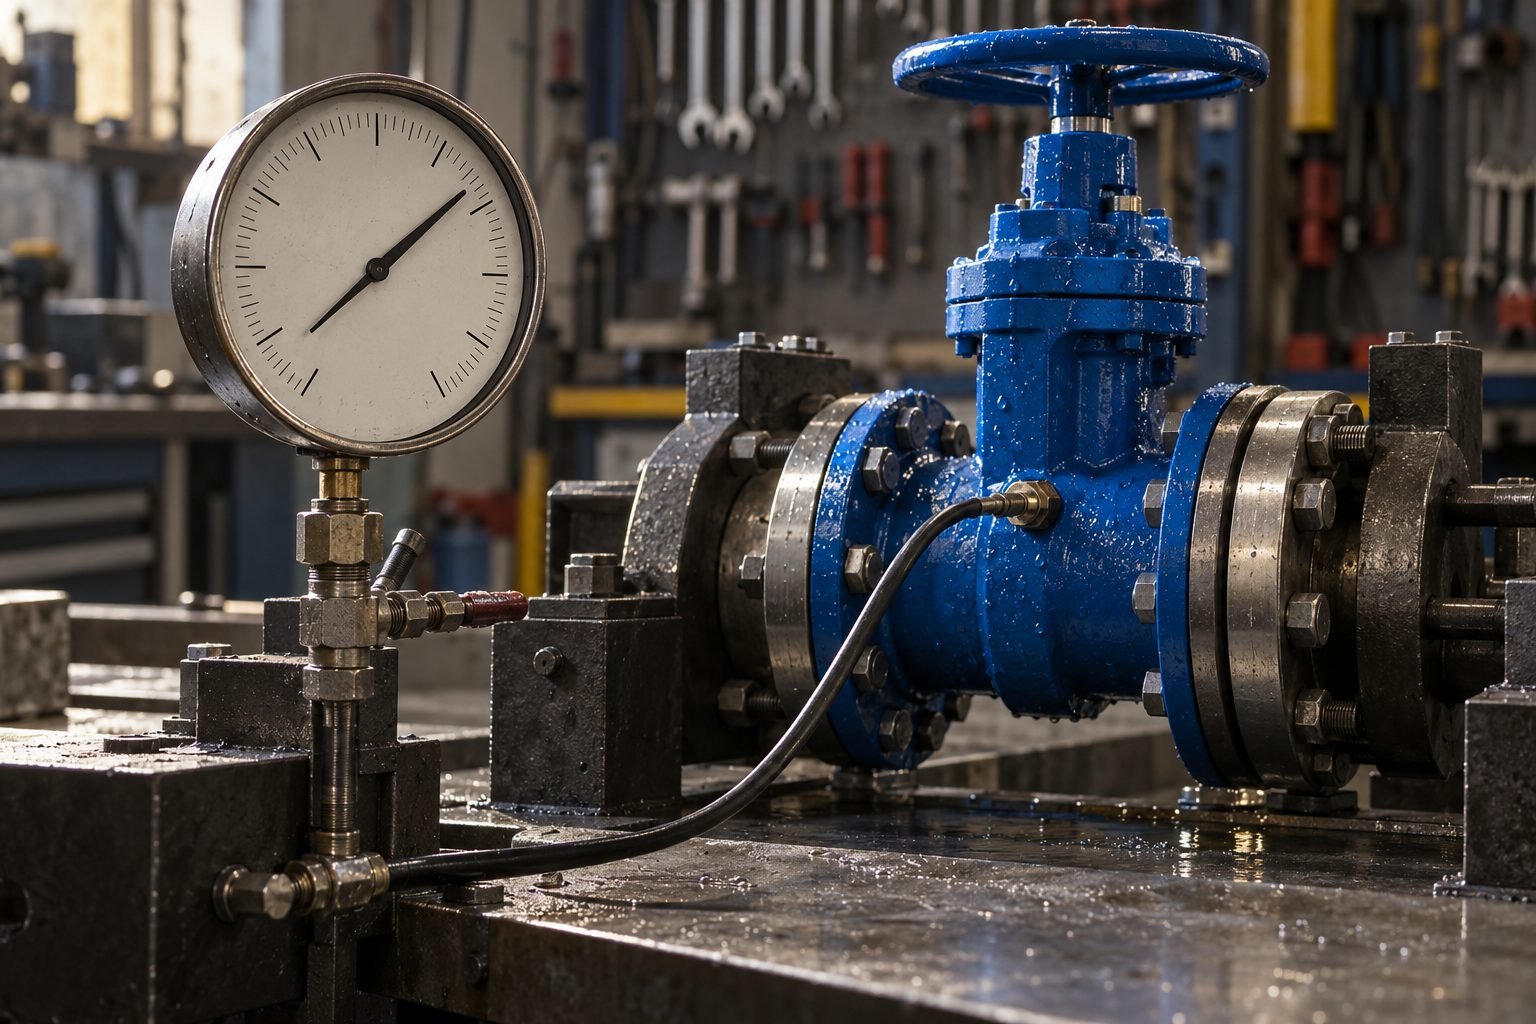
A test with clear criteria.
Specify shell and closure tests with standard, pressure, duration and leakage criterion. EN 12266-1 and API 598 are test references; applicability depends on the valve.
- Shell
- Strength and tightness
- Closure
- Seat and permitted leakage
Order the documents with the product.
Agree EN 10204 3.1 certificates, test reports or third-party inspection before production. Availability, scope and cost are confirmed with the factory.
- On request
- Material, tests and external inspection
- Shipment
- Packing list and agreed documents
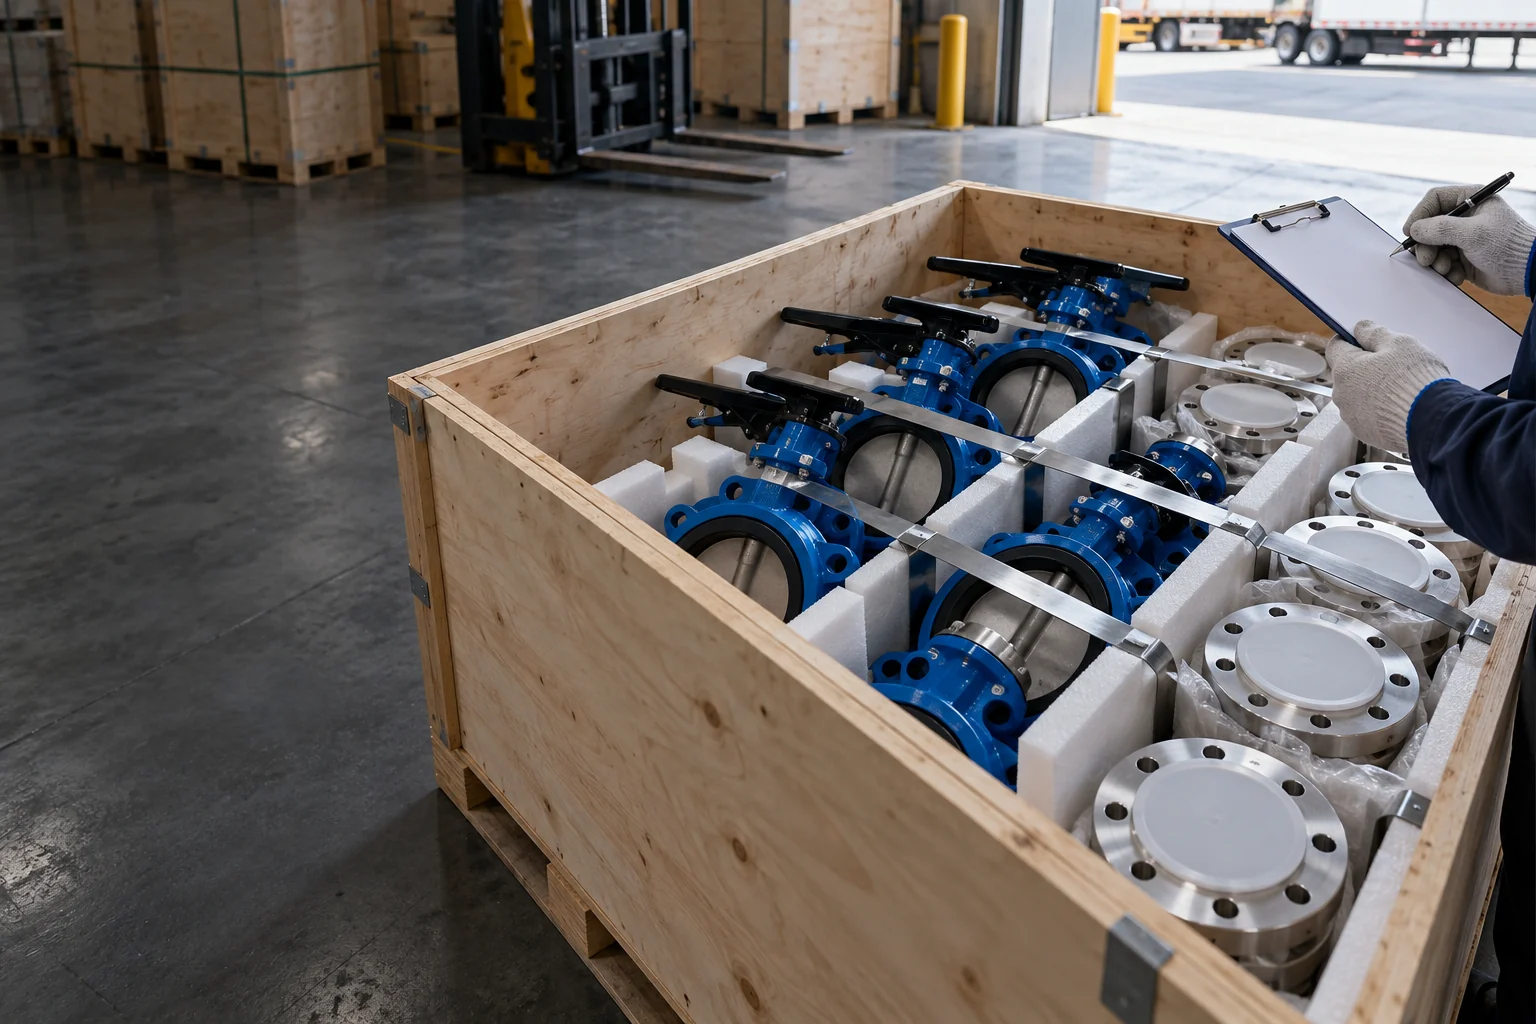
Protect each part to its destination.
Packing checks cover machined faces, pipe ends and small components. Agree package identification, quantities and protection to simplify receiving and installation.
- Protection
- Faces, ends and surfaces
- Receiving
- Packages identified against the list